


A titanium hip stem can break right where its serial number was laser etched. In one published series of 295 stems laser etched on the neck, 5.4% of necks fractured, and every fracture was fatigue.
Laser marking titanium is easy. Picking the right mark and putting it in the right place is the hard part.
Titanium is a regular in the HeatSign sample lab, and buyers ask the same questions every time. This guide covers the four mark types, what UDI and MIL-STD-130 ask for, where to mark load-bearing parts, which marks survive post-processing, and which machine to use.
Reusable surgical instruments
Black anneal
Data Matrix code plus plain text
Rule: FDA 21 CFR 801.45 permanent UDI
Implants
Implant spec first
Then ASTM F86 for surface prep and marking
Rule: mark in a low-stress zone
Aerospace and defense parts
Data Matrix ECC 200
Where the drawing says
Rule: verify the grade (MIL-STD-130, AS9132)
General industrial titanium
Deep engrave or dot peen
Tube sheets, flanges, fasteners
Why: survives blasting and paint
Know your mark type? See which machine fits, or send us your drawing.
What kinds of laser marks can you put on titanium?
There are four: a black annealed mark, a white frosted mark, a color oxide mark and a deep engraving. The first three change only a thin surface layer. Deep engraving removes metal, so keep it off load-bearing areas.
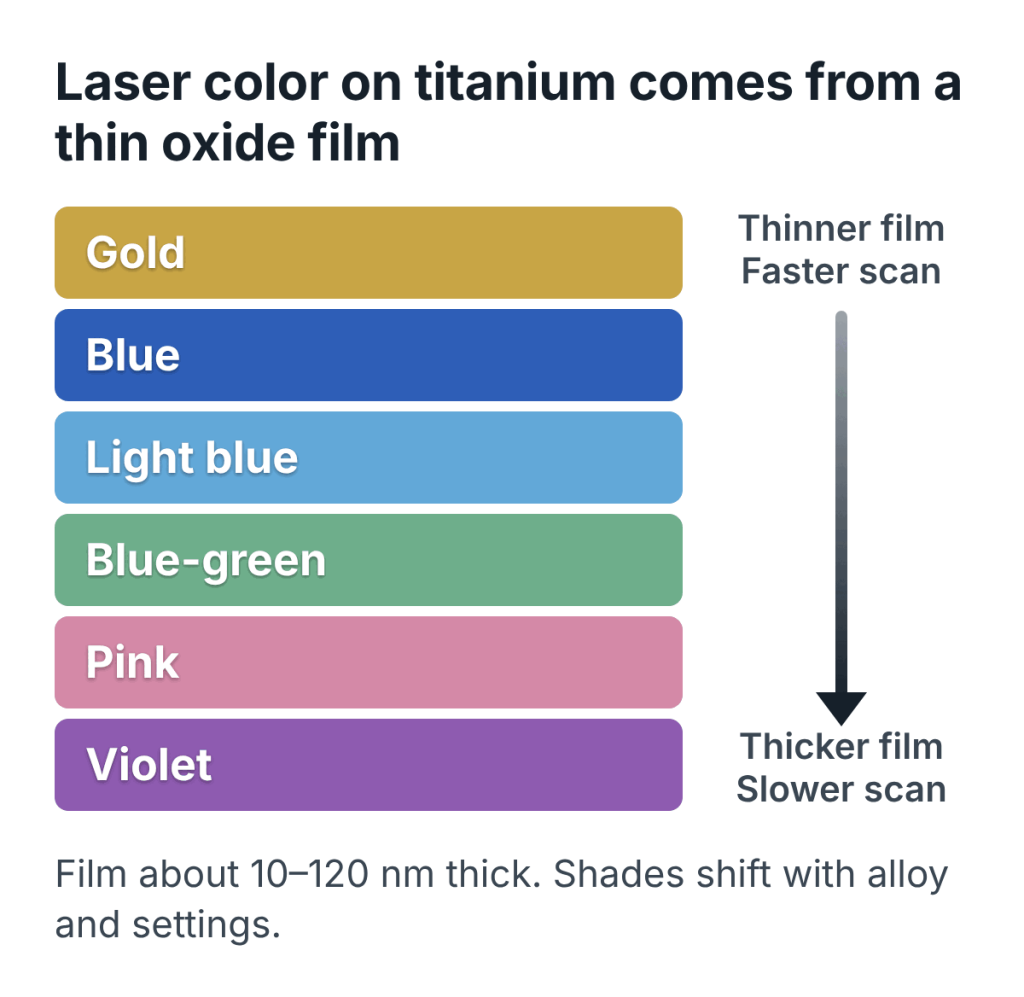
Annealing (heating the surface until it changes color) grows a clear oxide film on titanium. Sandia National Laboratories reports that the film thickens as the scan speed drops. Published measurements put laser-grown oxide on titanium at about 10–120 nm, far thinner than a human hair (about 70 µm). Light reflecting inside that film creates the color.
Mark | What changes on the surface | Depth | Best for |
|---|---|---|---|
Black anneal | Dark oxide film, no metal removed | Flush | UDI marks and serial numbers on instruments and load-bearing parts |
White frost | Very light texture, high scan speed | Near flush | Logos and QR codes on polished or dark surfaces |
Color oxide | Thicker oxide film; gold, blue, violet | Flush | Branding and kit colors; not for traceability marks |
Deep engrave | Metal removed in passes | 0.2–0.3 mm (0.008–0.012 in) or more | Parts that get blasted or painted; non-critical zones |
On the same HeatSign machine, the black mark uses lower speed, higher power and higher frequency, so the surface oxidizes. The white mark uses higher speed, lower power and lower frequency, so it only frosts the surface. In our test video, a fiber laser cut a 0.2–0.3 mm deep number into titanium in about 30 seconds.

For how annealing differs from etching and engraving on other metals, see our laser etching vs engraving guide.
Which machine marks titanium best?
For black, white and color marks, use a MOPA fiber laser (one that can change its pulse length). Its 2–350 ns pulse range lets you control heat on thin or polished parts. For deep engraving, a 30–50 W fiber laser works. HeatSign MOPA machines cost about $2,500–6,500.
 MOPA fiber laser, 30 / 60 / 100 W · $2,500–6,500Black and color annealing, white frost and fine Data Matrix codes on instruments and implants.See the MOPA laser engraver →
 Desktop fiber laser, 20–60 W · $1,950–5,000Deep engraving and serial numbers on titanium fasteners, tube sheets and brackets.See the desktop fiber laser →
 Pneumatic dot peen marker · $1,500–2,800Deep, low-cost marks on heavy, non-critical titanium parts.See the dot peen marker →
A dot peen marker (a carbide pin that punches rows of dots) is fast and cheap, but every dot is a small dent. Use it on flanges and brackets, not on fatigue-critical areas. A UV laser mainly makes sense for the top layer of anodized or coated titanium.
For machine setups and field size by part, see our titanium laser marking machine page.
What does UDI require on titanium surgical instruments and implants?
If a device is used more than once and reprocessed before each use, FDA rule 21 CFR 801.45 requires a permanent UDI on the device itself. It can be plain text, a machine-readable barcode or both. Implants follow their own spec and ASTM F86.
UDI means Unique Device Identification: the identifier that tells a hospital exactly which device and lot it holds. Most titanium instrument makers use a black annealed Data Matrix code (a small square barcode) plus a plain-text line. The rule text is in 21 CFR 801.45.
- Know the four exceptions. You can skip direct marking if any mark would harm safety or performance, or if it is not technically feasible. The other two cover some reprocessed single-use devices and devices already marked. Write the reason into your design history file.
- Check the implant spec first. ASTM F86 covers surface preparation and marking of titanium implants. Its purpose is “improving the corrosion resistance of the implant surfaces and markings.” A marking method in the implant spec overrides F86.
- Decide the order. F86 allows marking before or after surface treatment. If you mark after, assess whether the mark area needs treatment again.
- Do not passivate titanium to ASTM A967. A967 covers stainless steel only. For titanium cleaning and descaling, ASTM B600 is the guide.

The titanium grades themselves have implant standards: ASTM F67 for unalloyed titanium and ASTM F136 for Ti-6Al-4V ELI (the low-impurity grade of the common alloy). For UDI layouts and symbol sizes, see our UDI medical device marking guide.
Marking titanium instruments for UDI? Send us a sample instrument and we will mark and grade the code.
What do aerospace and defense specs ask for on titanium parts?
MIL-STD-130 requires a Data Matrix ECC 200 code with 0.19–0.635 mm cells, no larger than 25.4 mm (1 in). It must pass a verified grade, such as ISO/IEC TR 29158 DPM grade 2.0 or the AS9132 rules. The part’s design owner decides the location.
Requirement | What it says | Source |
|---|---|---|
Code type | Data Matrix ECC 200 only | MIL-STD-130N |
Cell size | 0.19–0.635 mm (0.0075–0.025 in); symbol up to 25.4 mm | MIL-STD-130N |
Quality check | ISO/IEC 15415 grade 3.0, or ISO/IEC TR 29158 grade 2.0, or AS9132 | MIL-STD-130N |
Location | Set by the company that designs the part | SAE AS9132 |
Restricted methods | Listed in AS478 and on the drawing | SAE AS478 |
MIL-STD-130 also lists marking methods. It describes laser discoloration as working “without associated metal removal.” Laser etching is “generally limited to 0.001 inch maximum depth” (0.025 mm). That is why most Data Matrix codes on aerospace titanium are annealed, not engraved.

For dot peen, laser and electro-chemical marking under the aerospace standard, read our AS9132 compliance guide. To learn how verifiers grade a Data Matrix code, see readable vs verifiable.
Need your titanium Data Matrix code graded? Send us the drawing and the spec you must meet.
Where should the mark go on a load-bearing titanium part?
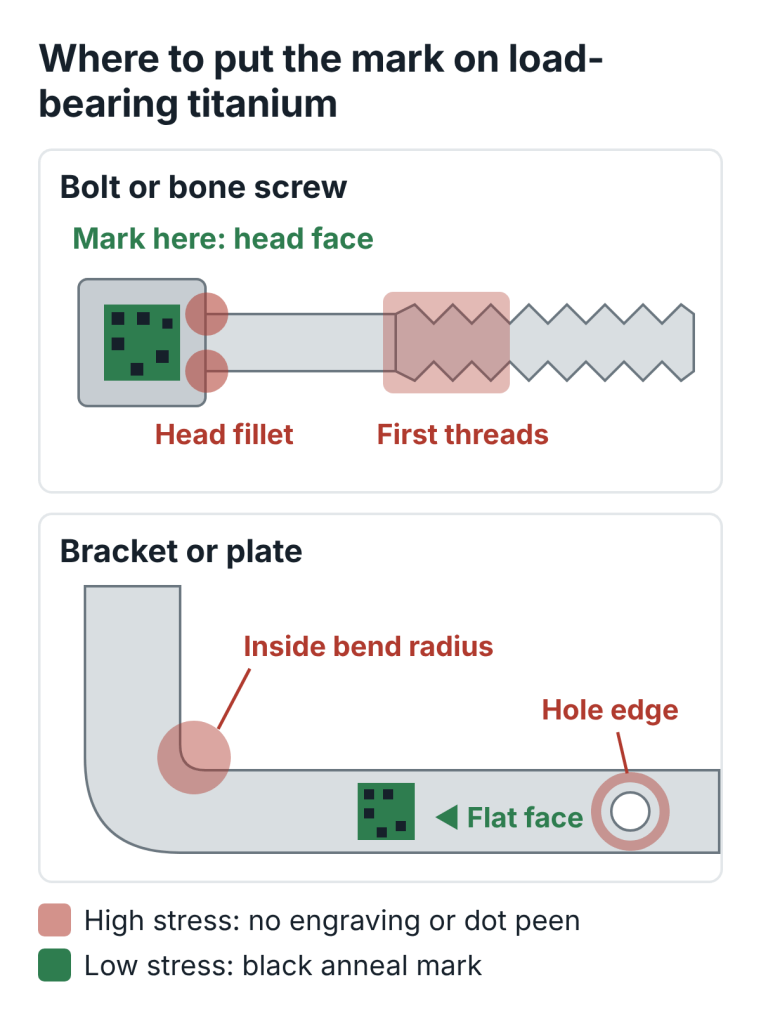
Put it in a low-stress zone, away from necks, thread roots and bend radii. On load-bearing parts, use a mark that removes no metal. In one Ti-6Al-4V test, a laser-marked part lasted 99,745 load cycles against 315,789 for an unmarked one.
Fatigue means cracks that grow after many load cycles, even below the part’s rated strength. An engraved groove or a peened dot is a stress riser: a small notch where the crack prefers to start.
Lab test
Ti-6Al-4V external fixator parts. The authors call it a limited study (one pair) and warn that “positioning of laser marking is highly critical.”
315,789 cycles unmarked vs 99,745 marked
Clinical
295 titanium hip stems etched on the neck. All fractures were fatigue fractures linked to the etching.
5.4% of necks broke
Body fluid
In simulated body fluid, laser treatment shortened the corrosion-fatigue life of commercially pure titanium and Ti-6Al-4V.
About 20% shorter life
The fix is cheap: move the mark. Ask the design owner for a low-stress pad or a flat area, and mark there with a black anneal.
Which titanium marks survive passivation, autoclaving and blasting?
Deep engraving survives blasting. Black annealed marks are the usual UDI choice, but public data on titanium marks after autoclaving is thin. Color marks fade first. So test your own part: mark it, run your real cleaning and sterilizing steps, then grade the Data Matrix code again.
Mark | Blasting | Chemical cleaning | Steam sterilizing |
|---|---|---|---|
Black anneal | ✗ Removed with the surface | ~ Test itno Ti data | ~ 500+ cycles on stainlessvendor |
White frost | ✗ Removed | ~ Test it | ~ Test it |
Color oxide | ✗ Removed | ✗ Fades firstvendor | ✗ Not for UDI |
Deep engrave | ✓ Stays | ✓ Stays | ✓ Stays (watch fatigue) |
The only sterilizing figure we found is for stainless steel, not titanium. A laser vendor study found high-contrast UDI codes resisted at least 500 sterilizing and cleaning cycles. Corrosion results on titanium also disagree: one study found lower corrosion resistance after laser treatment, another found the marked surface more stable.
Steam sterilizing usually means 121 °C (250 °F) for 30 minutes or 132 °C (270 °F) for 4 minutes, per CDC guidance.
- 1
Mark
Mark a sample of your real part with the production machine and settings.
- 2
Run your real process
Blasting, cleaning, passivation or sterilizing, with your cycle count.
- 3
Grade before and after
Use an ISO/IEC TR 29158 verifier. Keep the report in your validation file.

Want proof on your own part? Send HeatSign a sample part and your post-process steps.
What else do buyers ask about laser marking titanium?
Can you laser mark titanium without weakening it?
Yes, if the mark removes no metal and sits in a low-stress zone. A black annealed mark only grows a thin oxide film. Engraving and dot peen dents can start fatigue cracks, so HeatSign recommends them only for non-critical areas.
Does laser marking titanium affect corrosion resistance?
It can. One study found lower corrosion resistance in simulated body fluid after laser treatment, while another found the marked surface more stable. Because results differ, run your normal surface treatment after marking and verify the part.
What colors can a laser make on titanium?
Gold, blue, light blue, pink and violet, roughly in that order as the oxide film gets thicker. A MOPA laser controls the film through speed, power and pulse length. Color marks look good but fade first, so do not use them for UDI marks.
Not sure which mark your titanium part needs?
The two mistakes we see most: deep engraving a serial number on a stem neck or thread root, and using a color mark as the only UDI. Both look fine on day one and fail later.
Send HeatSign your drawing, the material grade and your post-process steps. We will mark samples on the matching machine and grade the Data Matrix code before you buy.
Sources
- US eCFR, 21 CFR 801.45: devices that must be directly marked
- ASTM F86, Surface Preparation and Marking of Metallic Surgical Implants; ASTM A967, B600, F67 and F136 (scope pages)
- MIL-STD-130N, Identification Marking of U.S. Military Property
- SAE AS9132 and AS478 (scope pages)
- Ogrodnik et al., laser marking and fatigue of Ti6Al4V fixation parts, Journal of Medical Engineering
- Merini et al., neck fractures in laser-etched titanium hip stems, Orthopaedics & Traumatology: Surgery & Research
- Gil et al., laser treatment and corrosion fatigue of titanium, Journal of Materials Science: Materials in Medicine
- Kosec et al., laser-marked titanium surfaces, Coatings
- US CDC, steam sterilization guideline






